Sunday, January 31, 2010

2010 Is Off To A Great Start

Welcome Back. Happy New Year, and thanks for stopping back to check in on us at Prowler Aviation. We are off to a really good start in 2010. Here are the bullets for this update:
1. CNC Jigs
2. Tailwheel Strut Fabrication
3. Airplane CAD Work
4. A Free 8 Foot Sheetmetal Brake
5. More Tools
6. Cabi Saves Kit #9 from the recycling SCRAP HEAP!!!
7. Bud's Airplane (Kit #16) Attempted First Engine Start
8. Chuck's Airplane (Kit #12) FLIES AGAIN
9. Ray's Airplane (Kit #10)

Here's the Latest:

1. CNC Jigs - We recently had to fabricate jigs for 2 parts that we have in the CNC process. To make production as simple, pratical, and repeatable as possible you have to find a way to hold the stock rigidly while the machine does it's thing. You also have to find a way to hold the stock without machine hitting something that it's not supposed to. So far we made jigs for the steel wing plates and the TW strut.

2. Tailwheel Strut Fabrication - is nearly complete. Bryan has asked to have a TW strut fabricated. His kit never had one and he's going to begin the fuselage soon and wanted to start lining up all the parts. So, as we've shown in previous posts, we did the CAD work for the TW strut and got the machining done. One of the steps in the process was CNC shown above (jigs). The bushing holes still need to be reamed and the bushing pressed into them - but the processes are now in place to make these parts in the future.


3. Airplane CAD Work - We've been working diligently on the CAD work for the airplane. We've finished the drawings for the Vert Stab, Horz Stab, Rudder, Elevator, Main Wing Spar, Outboard Wing Spars, Rear Spars, Torque Boxes. The measurements have been done for all of the Center Wing Framing Components and the Outboard Wing Framing Components. When the drawings are completed for these last two sections, we will have completed a CAD drawing for roughly 1/2 the airframe components. The next step in process will be to go back and assemble the individual components into sub-assemblies where appropriate.

4. A Free 8 Foot Sheetmetal Brake (Sort-of) - We got a line on an 8 foot sheetmetal brake that a gent in SoCal was giving away to a good home. It's not a complete sheetmetal brake, however, and needs a lot of TLC. The base of the brake and the bending fence are are what we've gotten, but it's missing the top parts that clamp the material while bending. With a bit of elbow grease and fabrication of some parts, it will become a servicable unit - for a lot less than purchasing one. So far we've taken possesion of the brake, transported it to the shop, taken it completely apart, stripped and sand-blasted all of the parts and then painted everything. The next time in the shop we'll get pieces all re-assembled and get a start of fabricating parts to build the top, clamping part of the brake. Here are pics of what it looked like on arrival:
Started the tear apart, cleaning, sandblasting and fixing:
Sandblasting (effective but VERY tedious and messy!): Painted Pieces ready to go back together:

5. More Tools - We ended up picking up a few more tools from the gent that gave us the sheet metal brake. One of the tools is a Tooling Cutter/Grinder. It's a machine to make precise angles to make and/or sharpen toolings for mills, lathes, etc. It was a good deal and it will be nice to have the capability. Here's a pic: Clean up and restoration of this tool is on the back burner for now. At least until we need to sharpen some tooling.

The other item we got was a 30" combination shear, press brake and sliproll. Here it is before cleaning: It was a great deal because it has one broken arm. Here it is after cleaning:Here's the CAD drawing for the Prowler Plasma to cut out a new arm. We should have it fixed up in no time. More later. One of the great things of building this company slowly is that we have the time to find these "diamonds in the rough" and polish them up. It saves a lot of $$$ - but it does take time. Since we are not in any huge hurry, we can use this process to position the company for financial soundness.

6. Cabi Saves Kit #9 from the recycling SCRAP HEAP!!! - Late last year Cabi completed tracking down the old Prowler Aviation's Kit#9. The kit had changed hands a few times after it had been purchased from George. Somehow Cabi tracked it to a local college that it had been donated to. It languished there for years and ended up stored in an old CONEX box container. The college was very close to selling it for the scrap aluminum value. Cabi got the kit for value of the scrap metal. What a deal! Nice work John. Here are some pix:


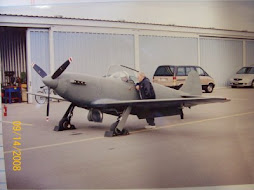
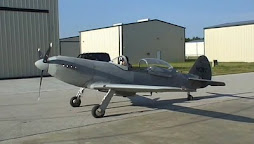
7. Bud's Airplane (Kit #16) Attempted First Engine Start - Got an email from Bud recently and he reported that he's attempted the first run-ups of his airplane. The engine didn't fire and after some investigation he found out that many of the silver solder joints on the fuel injection manifold had somehow become (essentially) closed off. So, he is in the process of making this right and we expect to hear good news from him soon. Here's a file pic of Bud's airplane from a visit last fall.

8. Chuck's Airplane (Kit #12) FLIES AGAIN - Last year Chuck was having engine troubles. The engine wasn't running real well, there were engine oil and water cooling issues - among other things. Chuck found a sharp fellow to help him tear the engine apart and find out what was going on. What they found was that one of the distributors was damaged and the engine appeared to be running in a severly "advanced" ignition timing condtion. This had badly damaged one pistion and somewhat damaged others. After many months of rebuilding, the airplane flew again in Jan. Chuck reports that the airplane flew well, the gear cycled well but the engine was not producing "linear" power. The engine ran great and "pulled like hell" at takeoff power, but as soon and the power was reduced, the engine power got "mushy" and difficult to control. He and his technician decided that there were some tuning issues between the mechanical fuel injection system, the supercharger system and the engine. They decided to remove the supercharger system from the airplane. After that, the engine ran great, the power was very controllable, and the airplane performed very, very well. Here's a pic of Chuck and his plane from a builder visit in 2008. In a later flight, the test pilot reported that the only remaining "gripe" was that at about 175 mph he ran out of elevator trim. So they will be focusing on getting the Horz Stab incidence set correctly in the near future. After that, Chuck says he will pay his pilot to fly off the 40 hours required to get the Experimental Certificate and then he will be putting the airplane up for sale. Stand by for more.

9. Ray's Airplane (Kit #10) - Is almost ready to get an engine - Ray reports being very close to completing the avionics installations in his airplane. He wants to get most of the wiring completed and get the avionics mostly complete before moving on to the engine and firewall forward. His goal is to get a good start on the engine mount and the the engine installed this year. Here is the most current pic we have of his instrument panel.
That's all for this update. More when additional info and time will allow. Thanks for stopping by.

Thursday, December 24, 2009

Happy Holidays From Prowler!

Hello again and welcome back again for the last post of 2009.

Well, this post is dedicated to only one thing - the Prowler CNC Plasma system. The past 2 weeks has been one last, large effort to get this system up and running and we're happy to report that it is - FINALLY!

Here's the report:

The first step in the last big push to get the system running was to get our shop compressed air up to par. Plasma torches use a fair amount of air and it needs to be clean and DRY! The old compressor didn't have the capacity to keep up the the almost 8 CFM of air required to of the PowerMax 1000 torch. A friend recently upgraded to a new larger compressor and we purchased his gently used unit. This machine stores 80 GAL of air and can provide 17.5 SCFM continuously @90PSI. More than enough to supply the current Prowler Shop. Once the unit was in position we needed to install a new regulator and plumbing to get the air directly to the torch in the most direct means possible. Here is the new piping and the tie-in to the existing manifold: Once we got the air over to the torch area, we finished the hook-ups to the refrigerated air dryer mentioned in the previous posts. The dry, clean air is critical to getting good cut quality. Here are shots of the torch cart (with the air dryer and computer card hook ups incorporated). The pic above also shows the new (used) computer we had to purchase for the CNC system. The previous computer was still having a problem running the control software (Mach3) and locking up the computer frequently. So we ordered a refurbished 3 Ghz P4 machine and loaded all the software onto it. We haven't had a problem running Mach3 since. With all that in place we were ready to start doing test cuts. Here is the first test cut: As you can see, it's not good. Lots of dross, very angular cuts, just a poor quality cut. After a while we got the cuts to improve a little, but they were still not good cuts. After several calls to Hypertherm and CandCNC we made a few tweaks and got the cuts to get a little better. But they still were not good. Something was still not right. At one point, a newly installed nozzle was blown off in 10 seconds of turning the torch on. Here are some pix of the carnage happening to the torch tips. This is not normal wear. Hypertherm recommended taking the PM1000 in for service. After removing the torch from the table and packing it down to the local welding shop the technician there noticed a few things about the modifications made to the hand torch that didn't seem right. He was right about one thing, and that made us go back and review the whole modification. Turns out that the biggest issue was that by mounting the brass "guts" of the hand torch in the aluminum wand (shown below); the nozzles were ultimately getting grounded through the table and essentially shorting out the torch. A few well placed rubber insulators got everything set right and we were able to start making good cuts. The part below is for the same friend that the air compressor came from. They are hooks to weld to the top of a tractor bucket. They're used for hooking up chains, straps, etc. for lifting or pulling. In any event, the torch is now able to cut 1/2" thick steel with pretty good cut quality. Our system does leave a small amount of angularity to the cuts on the 1/2" steel, but according to Tom of CandCNC, 1/2" steel is at the limit of the capability of a PM1000. If we wanted to get nice square cuts on this type material we'd have to upgrade to a much larger torch. But, since the thickest material we need to cut for the airplane is barely 1/4" - this system should work great for us. Here is a pic of the whole Prowler CNC plasma system: From here we must expand our plasma cutting knowledge to include using different types of nozzles, the 40Amp fine cut nozzles in particular. Also, we have to learn to cut some different types of materials for the airplane; mostly Chromoly Steel and Aluminum. We'll report on that in the New Year. We also have some interesting info for the next post on a long, lost kit that was saved from the scrap heap! Stop back again next year.

Merry Christmas and Happy New Year from us here at Prowler Aviation.

Sunday, November 29, 2009

A Little Slower - But Still Working

Welcome Back. We hope everyone enjoyed a Happy Thanksgiving this year. It's been a little bit slower paced around here lately, but we've still been working.
In this update:

1. Sheet Metal Brake Shoe
2. CAD Modeling
3. New Rotary Phase Converter Motor Stand
4. Plasma Torch Air
5. The Great Wall of Prowler


1. Sheet Metal Brake Shoe - In preparation to start bending a lot of sheet metal, we needed to modify our sheet metal brake to bend our aluminum with a radius. Standard sheet metal brakes come with fingers or shoes that will bend very sharp corners. Aluminum cannot be bent that sharply or it will crack between the metal grains. Most bends for Prowler Parts need 1/8" radius bends. So we needed to put the Bridgeport to use and make a shoe with a 1/8th" radius.


Now making hundreds of radius bends will be fast and easy with the modified brake. Should help speed up production. This covers the parts up to 4 feet. We've got another solution for parts over that length. Here's what the test piece looked like.

2. CAD Modeling - We've been using our CAD software to begin systematically modeling all of the parts and patterns for the Prowler. We learned to use the software while modeling a few of the parts (e.g. Tailwheel Strut) we've already mentioned in previous blog posts. But now we've begun to model all the parts in ernest. In the past two weeks we've completed the modeling of all the Vertical Stabilizer parts and the Horizontal Stabilizer parts. We're now starting on the parts for the center section of the main wing spar. BobCAD-CAM Ver. 23 was well worth the cost. Here's a sample of the software while modeling the Horz. Stab. skin.

3. New Rotary Phase Converter Motor Stand - While spending hours machining out the radius-ed shoe for the sheet metal brake, it became apparent that having the motor of the rotary phase converter mounted to a shelf on the wall behind the mill was not the best solution. The motor vibration was transmitted into the wall and amplified by the wall resonance. So, we used another of our new shop tools (MIG welder) to weld up a new motor stand that mounts to the concrete floor. It turned out great and the motor noise is substantially reduced.

4. Plasma Torch Air - We really need to get the plasma torch going. We're getting to the point where we really need to start cutting a lot of parts and we want to be able to use the plasma setup to do this - just like we will eventually be doing for production. We recently installed a new computer and the system is essentially set-up and tested. Here's a movie of the system cutting out a sample part we created (without the torch on):

The torch has tested fine as well, however, the weak link in the system is compressed air. Our air compressor did not have the capacity to keep up with the air required for the torch. In addition, the air cleaning/drying system we set up previously was not going to be adequate.

To solve the air supply problem we purchased a new (used) air compressor. Plans are in progress to find an acceptable to place to set up the air compressor outside of the shop. This will keep the noise down and make more room inside the shop. It will, unfortunately, require plumbing electrical out to the compressor and plumbing the air into the current manifold set up we have. Should be couple day project. More to follow.

To dry the air we purchased a new refrigerated air dryer and the torch cart has been modified to hold it. We still have to plumb the filter and the misc hookups. This project will be at the top of the list in the coming weeks.

5. The Great Wall of Prowler - Since the Prowler (West) shop was built we've been wanting to widen the driveway around the shop and add room to get in-and-out of the south garage door. We recently got access to a lot of broken concrete and fill from a job site. We transported it all to the shop and have begun to build a retaining wall around the front of the shop. It will give a lot more space for driveway and should help improve the look of the property. Unfortunately not everything can be directly related to building Prowlers!


That's it for this update. We'll update again when there is more to report. Thanks for stopping by.

Thursday, October 1, 2009

IT'S BEEN A BUSY MONTH!

Hello Again - It's been really busy this past month around the Prowler Shop. Included in this update:
1. Kit #13 Has a New Owner
2. Builder Visit w/ Bud Tedesco (Kit #16)
3. Redding Air Show
4. Bryan (Kit #007) Progress
5. Work on Tailwheel Struts
6. First Attempt At Bend Radius Jig
7. Added DRO to Bridgeport Mill Quill
8. Installed 3 Jaw Chuck on Lathe
9. Purchased a MIG welder

Overall, we're continuing to make progress on our first aircraft and Prowler the company. There is much to do to structure what we do now to make it repeatable in the future. Generally, when we work on the airplane we don't get much done on the company. And, when we work on the company, we don't get a lot done on the actual aircraft. But, all in due time. On with the update.

1. Kit #13 Has a New Owner - You may remember from our JAN09 post that Rick in Memphis purchased the RW&B aircraft (Kit #001) and also Kit #013 from the former owner in JAX. After reviewing and inventorying all of the parts, Rick decided to put Kit #013 up for sale. The kit was recently purchased by Roy Farris of Franklin, IN. Roy should take custody of the kit within the next few weeks. We'll pass along any new information once Roy gets his kit. Here's a couple of pix of Kit #013 taken when Rick was purchasing it earlier.


Congratulations Roy! We look forward to working with you in getting your airplane together and flying. Please send us your pix and your thoughts that we can share with everyone.

2. Builder Visit w/ Bud Tedesco (Kit #16) - On a recent trip to MCO for recurrent training, I was able to get up to Mount Dora, FL and visit Bud and see his aircraft. He's doing a fabulous job on it and is hoping to have it flying by the end of the year! Nearly all the systems have been installed and tested. He is currently working on installing all of the fairings and finishing up odds-n-ends. Here are a few pix of Bud's Beauty:


So far, Bud is the only builder that has incorporated a sliding canopy design into his Prowler. He came up with an ingenious design that allows it to work on a cockpit that is wider at the front than at the back. We'll look at incorporating this into our aircraft. BTW - that's Bud waving from the cockpit in the first picture above. Great job Bud - we'll keep tracking your progress. Hope you make your goal to have your aircraft fly this year.

3. Redding Air Show - The promoters of the Redding Air Show called George this year and asked him if he would, again, display his Prowler at the air show. He agreed and we spent Thurs before the airshow getting Kit #005 out of storage, towing it up to KRDD, putting the wings on, and giving it a much needed bath. This was our first opportunity to see how the airplane is taken on and off of the trailer, how the wings are put on and taken off, and enjoy seeing folks enjoy the airplane. There is now doubt about it - this airplane gets lots and lots of looks!
We may have gotten even more looks if it hadn't been 112F on the field that Saturday! It was hot, but it was a great show. Of Course, these guys always get the most looks!

4. Bryan's (Kit #007) Progress - A bit of a slowdown at work has allowed Bryan to really get some work done on his Prowler. He recently sent me a video of his flap operating system in operation. He chose an updated version of the electric linear actuator that George and others have used to operate the flaps. This design has a ball-screw drive with automatic clutching at each end. This negates the need for limit switches, provided that you get the correct stroke length. It does, however, require that a different mounting system be created to attach the fwd end of the actuator to the bulkhead. Here's a video:


http://www.blogger.com/video-play.mp4?contentId=76805bafaeb2cb07&type=video%2Fmp4

NOTE: Bryan also requested us to ask if there are any current builders out there that need the high tensile wing bolts - please contact us. He is going to order some of them and will order enough for everyone. These are sold only in lots of 10 (w/ certification paperwork). He will order enough to get everyone what they need and divide them up when received. Email us for details.

5. Work on Tailwheel Struts - We've ordered the stock material for the tailwheel struts and identified a machine shop to begin making these from our newly made drawings (see previous post). This is to support the current builders that are in need of these items. While we're at it, we'll make a couple extra struts - one for our aircraft and one for possible future needs. Here's an updated 3D version of the TW strut since we "tweaked" the design a little. We should have some new pix for the next update.

6. First Attempt At Bend Radius Jig - We made a first try at making a bending radius jig to make bending 2024-T3 in the box brake easier and faster to do. Since we have a lot of this type of forming to do now (and even more in the future) we are putting time into making these processes very quick and efficient so production can be as efficient as possible. So, we tried welding a 1/4" round stock to the edge of a 1/4" piece of flat bar to create a "jig" to lay on top of the material to bend in the brake. Unfortunately, the heat from the welding stitches caused the jig to warp and made it unusable. In addition, we found out the the top fingers on the brake cannot be adjusted back far enough to accommodate this design. So, we're on to "Plan B" and should have some more info and pix in the next update. If at first you don't succeed - try, try again.

7. Installed DRO on Bridgeport Mill Quill -
This project turned out much more successfully than the one mentioned above. For less than $40 (including shipping) we purchased one of these quill DRO's. It did not, however, come with the mounting hardware - so a little imagination and fabrication were in order. Here's what we came up with.We have one more idea to make this more practical and useful. More to follow.


8. Installed 3 Jaw Chuck on Lathe - Last year we purchased a older used lathe and restored it back to a usable condition. It came with a 4 inch 4 jaw chuck, but we need the convenience of a 3 jaw chuck so we purchased one from ENCO. Trouble was, this lathe is so old that no one makes a back plate for mounting the chuck (uses a 1-1/4" 12tpi fastener to thread onto the lathe spindle). So, we had to make one. First step is to weld a 1-1/4" 12 tpi nut to a piece of 1/2" plate that has a 1" hole cut through it.Next, put it on the lathe to true up the face and side. Also, cut a shoulder on the edge to give a raised area which will fit into a recess on the back of the chuck (ensures it is concentric when installed on back of chuck). Drill 3 holes to bolt the back plate onto the chuck: Install the back plate onto the chuck: Install the completed chuck and back plate onto the lathe.
The dial indicators says run-out is less than 0.003" from side to side (less than 0.0015" from center to OD of the chuck). Good to go! Eventually we'll get a bigger and better lathe and this will be converted and set up to make one or two specific parts. But for now, we can use it to make several of the aircraft parts as well as general shop work.

9. Purchased a MIG Welder-
To facilitate making many of the jigs, tooling and other items needed to produce Prowler parts we needed to purchase a MIG welder. After months of watching the local classified and craigslist we found the right package at a great price.It's already been put to good use and it welds great. Of course, all the weldments for the aircraft parts will all be TIG welded (which we will outsource to a qualified welder initally). However, eventually we hope to purchase a TIG welder and take welding courses to bring this part of production in house as well.

Those are the high points for this installment. Next post we'll have a more complete update on the status of all the builders and their aircraft. Thanks for checking in on us and look for a Halloween update.